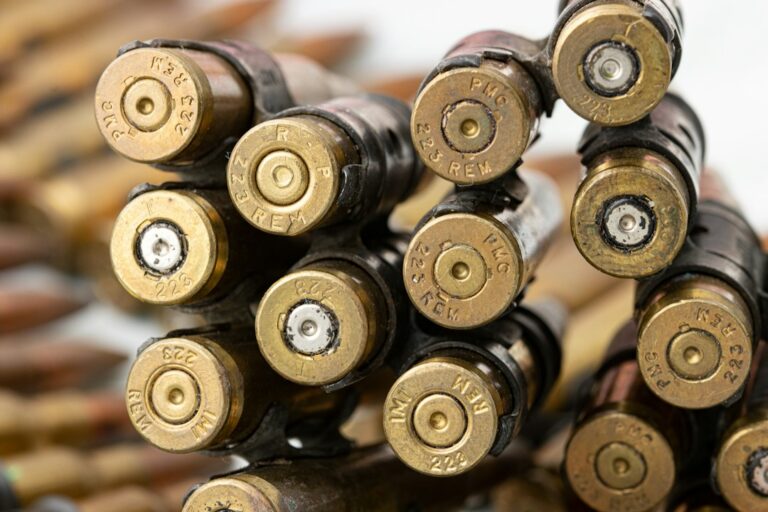
We approach the intricate world of .300 Winchester Magnum match ammunition with the respect it deserves, understanding that true precision at extended ranges begins long before the powder is charged or the bullet seated. Our journey into crafting exceptional .300 Win Mag rounds is an exercise in meticulous detail, where each step in case preparation contributes to the ultimate goal: unparalleled accuracy and consistency. The inherent power and ballistic capabilities of the .300 Win Mag make it a formidable contender in long-range competitions, and it’s this potential that drives our commitment to perfection in every brass casing we handle.
Selecting the Foundation: Brass Choice and Initial Inspection
Our initial foray into case preparation for .300 Win Mag match ammunition always begins with the most fundamental decision: the brass itself. We recognize that the quality of the raw material profoundly influences the final product. While factory-fresh brass offers the advantage of a clean slate, meticulously prepared once-fired brass can also yield excellent results. What we seek, above all, is consistency.
New Brass Considerations
When we opt for new brass, our primary focus is on manufacturers known for producing high-quality components. Brands like Lapua, Norma, Petersen, and even Hornady, with its emphasis on wall thickness uniformity, internal capacity, case weight, and concentricity for its 178 gr ELD Match ammunition, are often at the top of our list. The appeal of new brass lies in its virgin state, free from the stresses and strains of a previous firing. However, “new” does not automatically equate to “perfect.” We still subject new brass to a thorough inspection process. This includes visually checking for any dents, dings, or deformities that might have occurred during manufacturing or shipping. We also perform a quick run-out check on a selection of cases to ensure initial concentricity is within acceptable limits. While it might seem counterintuitive to process new brass, we find that even premium new brass benefits from a consistent regimen of neck sizing, chamfering, and deburring to optimize it for our specific dies and chambers.
Once-Fired Brass Protocol
For those times when we utilize once-fired brass, the selection and preparation process becomes even more critical. We prefer to use brass fired from our own rifle, as this brass has already been fire-formed to our chamber. This minimizes the need for significant reshaping during subsequent sizing operations and potentially reduces work-hardening. The source of once-fired brass is crucial; we avoid unknown origins or brass that shows signs of excessive pressure or damage.
Our first step with once-fired brass is a thorough visual inspection. We look for extractor marks, ejector smears, pressure rings, and any signs of impending case head separation. Any brass exhibiting these issues is immediately discarded. We then move on to cleaning. While ultrasonic cleaning is effective, we often tumble our brass in a vibratory tumbler with a media like crushed walnut or corn cob, sometimes with an added polish, to remove carbon fouling and bring back a clean, bright finish. This allows for easier inspection and better lubricity during sizing. After cleaning, we re-inspect each case for any flaws that may have been obscured by fouling.
Measuring and Sorting
Regardless of whether we start with new or once-fired brass, a critical step is measuring and sorting. We use a digital caliper to measure overall case length and discard any cases that are significantly out of spec (too short or too long). More importantly, we sort cases by headstamp and, if we have a sufficiently large batch, by weight. While not always strictly necessary for every casual reloader, for match ammunition, sorting by case weight helps us identify any significant variations in internal volume, which can lead to velocity deviations. The Hornady 178 gr ELD Match product page specifically calls out case weight as a factor in their factory match ammunition, underscoring its importance. We aim for lots where the weight variation is minimal, typically within a grain or two.
For those interested in enhancing their understanding of case preparation for .300 Win Mag match ammunition, a valuable resource can be found in the article titled “Precision Reloading Techniques for .300 Win Mag.” This article delves into the intricacies of reloading, including tips on case trimming, neck sizing, and primer selection, which are essential for achieving optimal accuracy. To explore this informative piece, visit here.
Precision Sizing and Neck Management
With our brass selected and initially prepared, we move into the crucial phase of precision sizing and meticulous neck management. This is where we impose uniformity and prepare the case for optimal bullet seating and consistent powder ignition. The goal is not merely to return the case to spec, but to achieve a precise fit within our chamber while minimizing brass fatigue.
Full-Length Sizing with Bushing Dies
For our .300 Win Mag match loads, we almost exclusively use full-length sizing dies with interchangeable bushings. While neck sizing dies can extend brass life, the .300 Win Mag’s powerful recoil and potential for chambering issues in semi-automatic or lever-action rifles often make full-length sizing a more reliable choice, especially in competitive scenarios where quick, unhindered feeding is paramount. Even for bolt-action rifles, we find that a consistent shoulder bump, achieved through full-length sizing, contributes to smoother chambering and more reliable feeding, which is critical under timed competition stress.
Our process involves setting up the full-length sizing die to bump the shoulder back a minimal amount, typically 0.001″ to 0.002″. This is measured using a comparator tool, ensuring we only push the shoulder back enough for reliable chambering without overworking the brass. We incrementally adjust the die until we achieve this precise shoulder bump. Lubrication is key here; we use a high-quality case lubricant, ensuring even coverage but avoiding excessive application, which can lead to dents or hydraulic lock.
The use of bushing dies allows us to fine-tune the neck tension. We experiment with different bushing sizes to achieve the ideal neck tension for our chosen bullet. This often means measuring the outside diameter of a loaded round and selecting a bushing that sizes the neck down approximately 0.002″ to 0.003″ smaller than the seated bullet’s diameter. This provides sufficient grip on the bullet without deforming it or causing excessive concentricity issues. We always deburr and chamfer the flash hole on new brass and ream or uniform primer pockets if necessary after sizing to ensure uniform ignition.
Neck Turning for Uniformity
For the utmost in precision, particularly with very light or heavy bullets where concentricity is paramount, we undertake neck turning. This process involves precisely machining the outside diameter of the case neck to achieve uniform wall thickness around the entire circumference. Hornady’s emphasis on wall thickness uniformity for its match loads, especially the 178 gr ELD Match, directly highlights the importance of this step.
We start by measuring the neck wall thickness at several points around the circumference of a selection of cases. If we find significant variations (more than 0.001″), neck turning becomes a high priority. We use a specialized neck turning tool, ensuring it’s properly set up to remove only the necessary amount of brass to achieve uniformity. The goal is to create a perfectly concentric neck that allows the bullet to be seated without any deflection, thereby promoting a perfectly aligned bullet flight path. This is a time-consuming process but one that yields tangible benefits in terms of reduced run-out and improved accuracy.
Flash Hole and Primer Pocket Uniforming
While sometimes overlooked, uniforming the flash hole and primer pocket contributes significantly to consistent ignition. For both new and once-fired brass, we inspect and often uniform the flash hole. This involves using a small, specialized tool to ream out any burrs or inconsistencies left over from the manufacturing process. A clean, uniform flash hole ensures a consistent flame path from the primer to the propellant, leading to more uniform pressure curves and velocities.
Similarly, we uniform the primer pockets. This involves using a primer pocket reamer or uniformer to ensure the primer pocket depth is consistent across all cases and that the bottom is perfectly flat. This allows the primer to seat firmly and consistently, promoting reliable ignition and reducing velocity variations. SIG Sauer’s emphasis on “premium primers” and “optimized shell-case metallurgy” to reduce velocity variation in their match-grade .300 Win Mag load reinforces the importance of this often-underappreciated aspect of case preparation. We aim for a consistent primer seating depth that provides a slight crush fit, indicating proper contact with the bottom of the primer pocket.
Trimming and Chamfering for Bullet Seating
Our meticulous journey continues with the critical steps of trimming the cases to a uniform length and then preparing the case mouth for seamless bullet seating. These seemingly minor operations play a surprisingly large role in overall accuracy and consistent performance.
Consistent Case Length
Maintaining a consistent case length is non-negotiable for match-grade ammunition. Variations in case length can lead to inconsistencies in bullet seating depth, crimp (if applied), and even internal case volume, all of which directly impact chamber pressure and velocity. We typically trim our .300 Win Mag cases to a length slightly below the maximum specified length, often around 2.610″ to 2.615″. This provides a small buffer before cases become too long and allows for several reloads before needing re-trimming.
We use a high-quality, precise case trimmer, often one that holds the case by the shoulder for greater consistency. After resizing, we measure each case individually. Any case exceeding our target length is trimmed. For new brass, we find that a significant number of cases might require initial trimming to bring them within our desired range. For once-fired brass, the brass will stretch with each firing, making regular trimming essential. We aim for a consistent final length, typically within a tolerance of +/- 0.001″. This ensures that each bullet is seated to the same relative depth within the case, contributing to consistent jump to the lands and, ultimately, consistent velocity.
Chamfering and Deburring
Once trimmed, the case mouth requires careful attention. The trimming process invariably leaves a burr on both the inside and outside edges of the case mouth. Failing to remove these burrs can lead to several problems:
- Bullet Damage: Sharp edges on the case mouth can scrape, deform, or even cut the bullet jacket during seating, leading to concentricity issues and reduced accuracy.
- Inconsistent Seating: Burrs can hinder smooth bullet seating, leading to variations in seating force and depth.
- Brass Fatigue: Sharp edges can accelerate cracking of the case mouth, particularly during subsequent firings.
We use a dedicated chamfering and deburring tool, often a VLD (Very Low Drag) chamfering tool for the internal chamfer, which creates a slight funnel shape to guide the bullet smoothly. The internal chamfer should be just enough to allow the bullet to start easily without excessive force. For the external deburr, we carefully remove any burrs from the outside edge of the case mouth, ensuring a smooth, clean surface. We take care not to remove too much material, as this can thin the case mouth excessively, potentially affecting neck tension. This step is performed on every case after trimming, ensuring each receives the same precise treatment for optimal bullet seating.
Cleaning and Final Inspection
Having meticulously shaped and prepared our brass, we now turn our attention to the crucial final stages of cleaning and inspection. These steps ensure that no contaminants remain and that every case meets our rigorous standards for match-grade ammunition.
Post-Processing Cleaning
Even after initial cleaning and the various processing steps, brass can accumulate residue from lubricants, metal shavings from trimming or neck turning, and even fine brass dust. These contaminants, if left in the case, can interfere with powder ignition, affect powder charge consistency, or even cause issues during firing. Therefore, a thorough post-processing cleaning is essential.
Our preferred method for this stage is ultrasonic cleaning with a specialized brass cleaning solution, followed by a rinse in distilled water. The ultrasonic cleaner effectively dislodges microscopic particles and lubricant residue from all surfaces, including the flash hole and primer pocket, which are difficult to clean otherwise. After the ultrasonic bath and rinse, we thoroughly dry the cases. This is typically done using a case dryer or by spreading them out on a clean towel and allowing them to air dry for an extended period, sometimes with the aid of a fan. Ensuring the cases are completely dry is paramount to prevent water contamination of powder and primers. Alternatively, for those without an ultrasonic cleaner, a final tumble in clean, dry media can also be effective in removing fine dust and polishing the cases.
Final Visual Inspection
Before any powder or primer touches our cases, we conduct a stringent final visual inspection of each and every piece of brass. This is our last opportunity to catch any overlooked defects or issues that might have arisen during the processing. We look for:
- Dents and Deformities: Any signs of damage that could compromise case integrity or affect chambering.
- Cracks: Especially around the case mouth or shoulder, which could lead to gas leaks or case separation.
- Primer Pocket Condition: Ensuring pockets are clean, uniform, and free of any debris or damage.
- Flash Hole Clarity: Confirming a clear, unobstructed flash hole.
- Consistent Case Mouth: Checking for any remaining burrs or uneven chamfering that might affect bullet seating.
- Lubricant Residue: Verifying that all lubricant has been removed, particularly from inside the case and primer pockets.
Any cases that fail this final inspection are immediately culled from the batch. Our philosophy is that a single compromised case can ruin a match, and the time invested in a thorough inspection is a small price to pay for confidence in our ammunition.
Run-Out Measurement and Sorting
For our most critical match loads, we take an additional step: measuring case neck run-out. After all sizing and processing, but before bullet seating, we use a concentricity gauge to measure the run-out of the case neck relative to the case body. While neck turning helps, some minor run-out can still be introduced during sizing. We aim for minimal run-out, ideally less than 0.002″. Cases with excessive run-out are either re-processed (if the issue is minor and identifiable) or discarded. This meticulous check ensures that our cases are perfectly straight, providing the ideal foundation for seating a perfectly aligned bullet. The goal here aligns with Hornady’s commitment to case concentricity in their factory match loads, emphasizing that it’s a quality marker we strive to replicate or exceed in our handloads.
When preparing cases for .300 Win Mag match ammunition, it’s essential to understand the intricacies of reloading and case preparation techniques. A related article that delves deeper into the specifics of this process can be found here: case preparation tips. This resource provides valuable insights into optimizing your ammunition for precision shooting, ensuring that every round is crafted to meet the highest standards of accuracy and consistency.
Practical Considerations and Long-Term Maintenance
| Metric | Specification | Recommended Value | Notes |
|---|---|---|---|
| Case Length | Maximum | 2.035 inches (51.7 mm) | Trim cases to maintain consistent length |
| Case Neck Thickness | Ideal Thickness | 0.014 – 0.016 inches | Uniform neck thickness ensures consistent bullet tension |
| Case Weight | Average | Approx. 180 grains | Sort cases by weight for consistency |
| Primer Pocket Diameter | Standard | 0.175 inches | Clean and uniform primer pockets improve ignition |
| Case Capacity | Approximate | 72 grains of water | Consistent capacity affects powder charge and pressure |
| Case Tumble Cleaning | Method | Wet tumbling with stainless steel media | Removes debris and polishing cases for better seating |
| Case Annealing | Recommended | After 5-7 firings | Prevents case neck cracking and improves consistency |
| Case Neck Turning | Recommended | Yes | Ensures uniform neck thickness for better accuracy |
| Deburring and Chamfering | Recommended | Yes | Prevents bullet damage and ensures smooth seating |
| Case Priming | Primer Type | Large Rifle Match Primer | Consistent ignition for match-grade loads |
Crafting match-grade .300 Win Mag ammunition is an ongoing process, not a one-time event. Our approach incorporates practical considerations and a commitment to long-term brass maintenance to ensure consistent performance over multiple reloading cycles.
Monitoring Brass Life and Fatigue
The .300 Win Mag is a powerful cartridge, and while modern brass is robust, it is subject to work hardening and fatigue with each firing and resizing cycle. We meticulously track the number of firings for each batch of brass. After every few firings (typically 3-5, depending on the load and brass manufacturer), we conduct an even more thorough inspection. We pay close attention to the internal base of the case using a paperclip or a specialized tool to detect any signs of incipient case head separation, which often manifests as a thinning or groove inside the case just above the web. Any cases showing these signs are immediately retired. We also watch for cracks in the neck or shoulder area, which indicate that the brass has reached its limit. While Barnes’ Precision Match emphasizes “factory-fresh brass” for consistent feeding and reloadability, our careful preparation and monitoring allow us to extend the useful life of our brass without compromising safety or accuracy.
Storage and Handling
Proper storage of prepared brass is crucial to preserve its integrity and cleanliness. We store our prepped cases in clearly labeled, airtight containers, away from temperature and humidity extremes. This prevents contamination from dust, moisture, and ensures the brass remains in optimal condition until it’s ready for the next loading steps. We also ensure that our storage solutions prevent any damage to the case mouths or shoulders during handling. Mishandling can easily negate hours of meticulous case preparation.
Environmental Factors and Propellant Stability
While not strictly case preparation, we recognize that the effectiveness of our precisely prepped cases is intrinsically linked to other components. The .300 Win Mag, being a cartridge often used in varying weather conditions, benefits greatly from temperature-stable propellants, a feature highlighted in Barnes’ Precision Match listing. When selecting powder for our loads, we prioritize those known for their stability across a wide temperature range. This means that even with a perfectly prepped case, the velocity and pressure characteristics will remain consistent whether we are shooting in cold mountain air or a warm desert environment. Our cases are prepared to offer the most consistent platform, and selecting stable propellants ensures that this consistency translates directly to the firing line.
Continuous Improvement and Data Collection
Our commitment to excellence in .300 Win Mag match ammunition means we are constantly learning and refining our techniques. We maintain detailed reloading logs, documenting every aspect of our case preparation, component choices (including different bullet weights like Hornady’s 195 gr ELD-M at 2,930 fps or 178 gr ELD-M at 2,960 fps, often recommended in the 190–220 grain range for long-range match applications), and performance outcomes. This data allows us to identify what works best for our specific rifles and conditions, and to make informed adjustments to our case preparation protocols. For instance, if we notice a sudden increase in case neck run-out after a specific number of firings, it might indicate that our resizing die needs adjustment or that the brass is nearing the end of its life. This iterative process of preparation, firing, data collection, and refinement ensures that our .300 Win Mag match ammunition continues to perform at the highest possible level, consistently delivering precision downrange. The ongoing pursuit of minimal velocity variation, as addressed by SIG Sauer’s use of optimized shell-case metallurgy and premium primers, is a shared goal that drives our every decision in the reloading process.
FAQs
What is .300 Win Mag match ammunition used for?
.300 Win Mag match ammunition is primarily used for long-range shooting and competitive shooting events. It is favored for its high velocity and flat trajectory, making it suitable for precision shooting at extended distances.
What are the key components of .300 Win Mag match ammunition?
The key components of .300 Win Mag match ammunition include the cartridge case, primer, powder, and bullet. The cartridge case is typically made from brass, the primer ignites the powder, and the bullet is designed for accuracy, often featuring a boat-tail design for improved aerodynamics.
How should cases be prepared for reloading .300 Win Mag match ammunition?
Case preparation for reloading .300 Win Mag match ammunition involves several steps: cleaning the cases to remove dirt and debris, resizing the cases to ensure proper fit in the chamber, trimming the cases to uniform length, and deburring the case mouths to prevent damage to the bullet during seating.
What is the importance of case neck tension in .300 Win Mag match ammunition?
Case neck tension is crucial in .300 Win Mag match ammunition as it affects bullet retention and consistency during firing. Proper neck tension ensures that the bullet is held securely in place, which contributes to uniform ignition and improved accuracy downrange.
How can I ensure consistency in my .300 Win Mag match ammunition?
To ensure consistency in .300 Win Mag match ammunition, it is important to use uniform components, maintain consistent loading techniques, and perform thorough case preparation. Additionally, using a reliable scale for measuring powder charges and conducting regular quality checks can help achieve consistent performance.